Gladiator GM Series

BUILT TO KEEP YOUR BORE MOVING

Gladiator Mud Systems deliver the mixing capacity, fluid consistency and jobsite reliability HDD crews need to stay productive. From compact support units to high-capacity systems, each model is designed for efficient mixing, circulation and delivery of drilling fluid in demanding conditions.

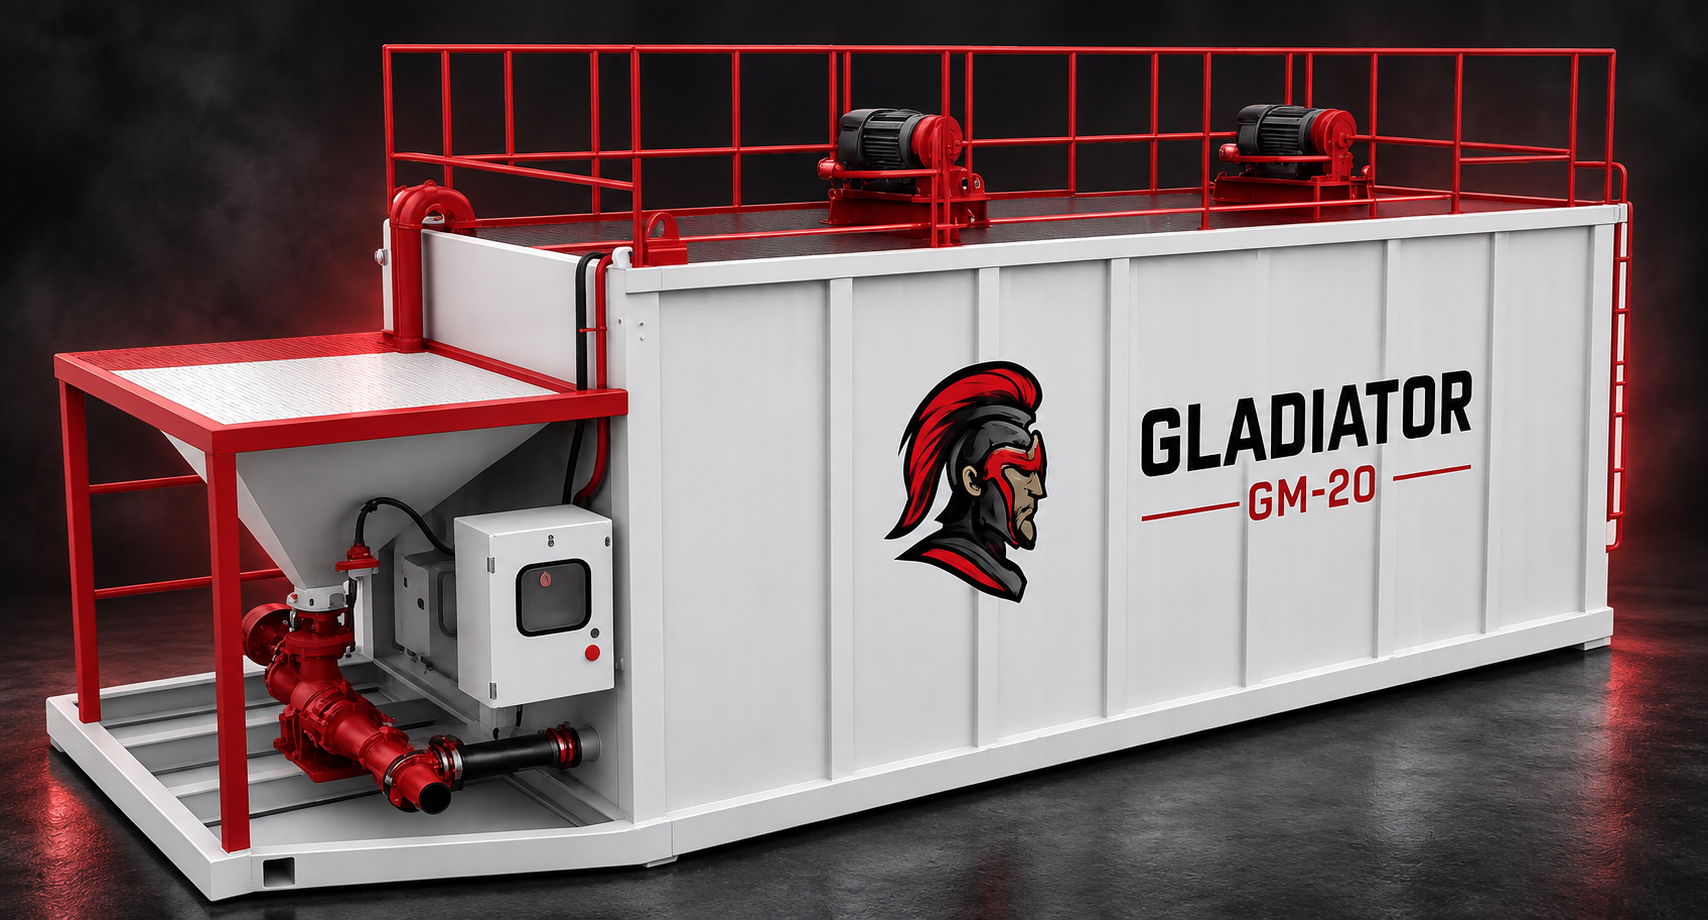
Large industrial container labeled Gladiator GM-20 in black and red text, featuring a gladiator helmet logo in red and black, with red railings and two black and red motors on top, and a red and white metal frame with pipes on one end.

Mixing and recycling. Two different jobs.

Choose a mixing system to prepare drilling fluid or a recycling package to remove solids from returned mud. Match the equipment to the fluid program, jobsite layout and required capacity.

GMR-600 Mud Recycling System

A skid-mounted, modular mud recycling package combining a shale shaker, desander, desilter, pumps and a four-compartment process tank.

  • Processing capacity: 600 GPM / 2,271 L/min / 136 m³/h
  • Approximate tank volume: 17.7 m³ / 4,676 gallons
  • Four tank compartments: 4.0 / 4.7 / 4.7 / 4.3 m³
  • Integrated access stairs, rails, lighting and control cabinet

Separate coarse and fine solids through successive treatment stages, with service access around the primary separation modules.

GMR-600 technical specifications (PDF)Request a quote →
GM-20 Mud Mixing System

Prepare and circulate drilling fluid with a two-compartment mixing system, high-shear hopper and dedicated pumping equipment.

  • Total tank volume: 20 m³
  • Mixing compartment: 9 m³; suction compartment: 11 m³
  • Two 7.5 kW agitators, one per compartment
  • 22 kW jet mixing pump; 120 m³/h flow
  • Mud transfer pump included
  • Electrical supply: 440 V / 60 Hz

Standard and extended-length configurations are listed. Confirm the required configuration and site layout with Gladiator.

Discuss the GM-20 →